Multi-Cavity Injection Molds: How to Solve Filling Imbalances & Boost Efficiency
In high-volume manufacturing, a stable multi-cavity injection mold determines your product consistency, cycle times, and per-part cost. At our Shanghai precision toolroom, we design and build high-end, high-cavitation molds that deliver uniform melt flow, precise thermal control, and long-term production reliability.
Core Engineering Specifications
We build complex multi-cavity tools tailored to strict global standards for automotive, medical, and consumer electronics applications:
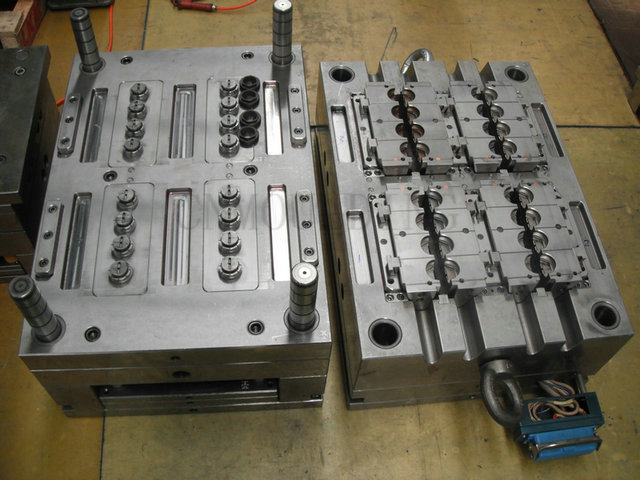
- Cavitation Capacity: From 2, 4, 8, 16 cavities up to high-volume 120-cavity molds.
- Modular Insert Construction: Using precision main and sub-inserts. Custom core/cavity pins with dedicated gas vent lands along the parting line eliminate air traps and burn marks.
- Premium Mold Steels: Through-hardened H13, 1.2344, 1.2312, P20, or 718H, selected specifically for your production volume.
- Advanced Heat Treatment: Hardening to HRC 52-54, plus specialized nitriding or coatings to resist wear and corrosion.
- Global Standard Components: 100% compatible with YUDO, DME, HASCO, and LKM hot runner systems and standard parts.
- Advanced CAE/CAD Support: Full flow and structural simulation using UG (NX), Creo, SolidWorks, and AutoCAD.
The Core Challenge: Why Multi-Cavity Filling Imbalances Happen
Achieving a balanced fill across every cavity is essential for maintaining a high CpK, holding micron-level tolerances, and ensuring identical part weights. Even a slight flow variance during filling leads to downstream problems like flashing, short shots, or dimensional warping.
Through rigorous DFM and Mold Flow analysis, we systematically eliminate the 7 root causes of multi-cavity filling imbalances:
1. Melt Temperature Inconsistencies
Unevenly heated polymer alters plastic viscosity and disrupts the flow front. For cold runners, we optimize barrel and nozzle thermal profiles. For hot runners, we use precise manifold and hot tip temperature zoning to prevent localized temperature drops.
2. Poor or Non-Uniform Venting
As plastic enters the cavities, trapped air and gas create backpressure. If venting varies across the layout, certain cavities face higher resistance and slow down.
- Our Solution: We run short-shot studies (comparing 65-80% fill vs. 90%+ fill) to isolate venting resistance from runner issues and fine-tune venting land depths.
3. Asymmetric Cooling Circuits
If cooling is uneven, plastic freezes at different rates across cavity plates, changing the effective flow channel. We avoid laminar flow and dead zones by designing high-turbulent cooling circuits with independent temperature regulation for critical tool zones.
4. Part Geometry & Wall Thickness Transitions
Sudden shifts between thick and thin sections cause the flow front to hesitate. We work with your product designers early to optimize nominal wall thickness and smooth out transitions—especially vital for living hinges and thin-walled packaging.
5. Shear Rate & Velocity Fluctuations
Varying fill times change the plastic’s shear rate and, consequently, its viscosity. We lock in precise, repeatable injection speeds and fill times across your molding machines to stabilize the material’s rheological behavior.
6. Micro-Variances in Gate Land Length
Even if gate diameters look identical, tiny differences in gate land length drastically alter pressure drops. We use high-precision EDM and CNC machining to guarantee identical gate land tolerances for every single gate.
7. Flawed Runner Layouts
Asymmetrical “ladder” layouts naturally cause filling imbalances. For high-precision multi-cavity tools, our default standard relies on naturally balanced runner layouts (such as H-patterns or radial designs) so every cavity shares the exact same flow distance from the main sprue.
Partner With Our Shanghai Toolroom
Don’t let multi-cavity imbalances drain your manufacturing profits. Partner with an experienced Shanghai mold maker that combines advanced flow simulation with micron-level machining. We solve potential tooling issues on the screen before cutting any steel—ensuring your high-volume production runs smoothly from T1 sampling to mass manufacturing.